
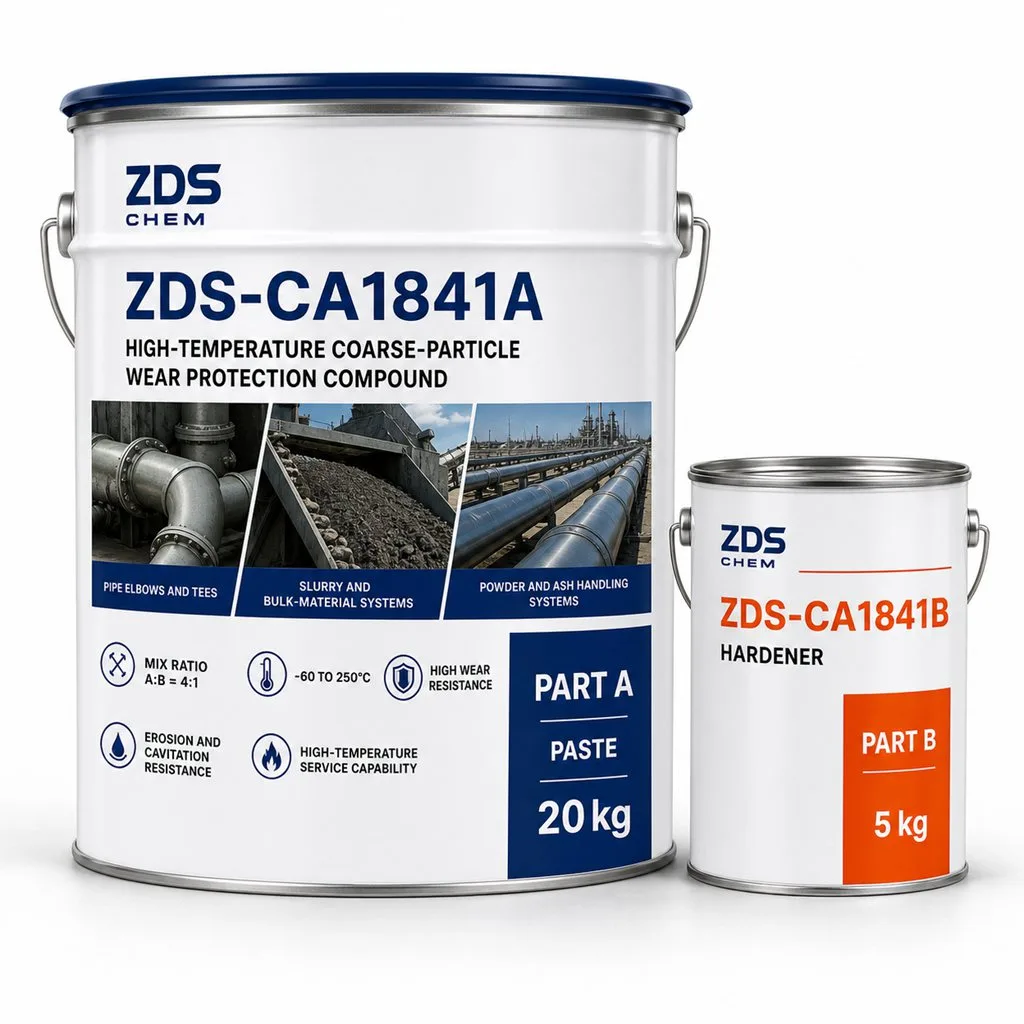
ZDS-CA1841
ZDS-CA1841 High-Temperature Coarse-Particle Wear Protection Compound
ZDS-CA1841 protects pipe elbows, tees and industrial pipeline areas from coarse-particle wear. It combines wear resistance with erosion, cavitation and high-temperature service capability.
Product overview
Coarse-particle wear protection
ZDS-CA1841 is a paste protective coating for pipe elbows, tees and industrial pipeline areas exposed to coarse-particle wear. It is suited to slurry, powder, ash and bulk-material handling equipment.
High wear resistance helps address repeated surface loss from abrasive flow. Erosion and cavitation resistance matter when fluid or particle movement is part of the damage mechanism. Its high-temperature service capability also helps when the coated component operates across changing industrial temperatures.
Key material properties
- Wear resistance: A useful property when selecting material for worn industrial surfaces.
- Erosion and cavitation resistance: Identify the actual damage mechanism when selecting the repair material.
- Temperature capability: Compare the service-temperature limits in the table with the operating conditions.
Evaluate the material
ZDS-CA1841 technical specifications
| Property | Value / conditions |
|---|---|
| Product model | ZDS-CA1841 |
| Product series | ZDS-CeramicArmor |
| Product family | Wear & erosion protection |
| Substrates and equipment | Pipe elbows and tees, slurry and bulk-material systems, powder and ash handling systems, industrial pipelines |
| Form and color | Paste; Typical: Dark grey |
| Working time at 25°C | Typical: 30-45 min |
| Initial cure at 25°C | Typical: 4-6 h |
| Full cure / cure conditions | 24 h |
| Service temperature | -60 to 250°C |
| Recommended application temperature | Recommended: 10°C to 35°C |
| Recommended application thickness | Recommended: 3-10 mm |
Questions about your operating conditions?
Where to use it
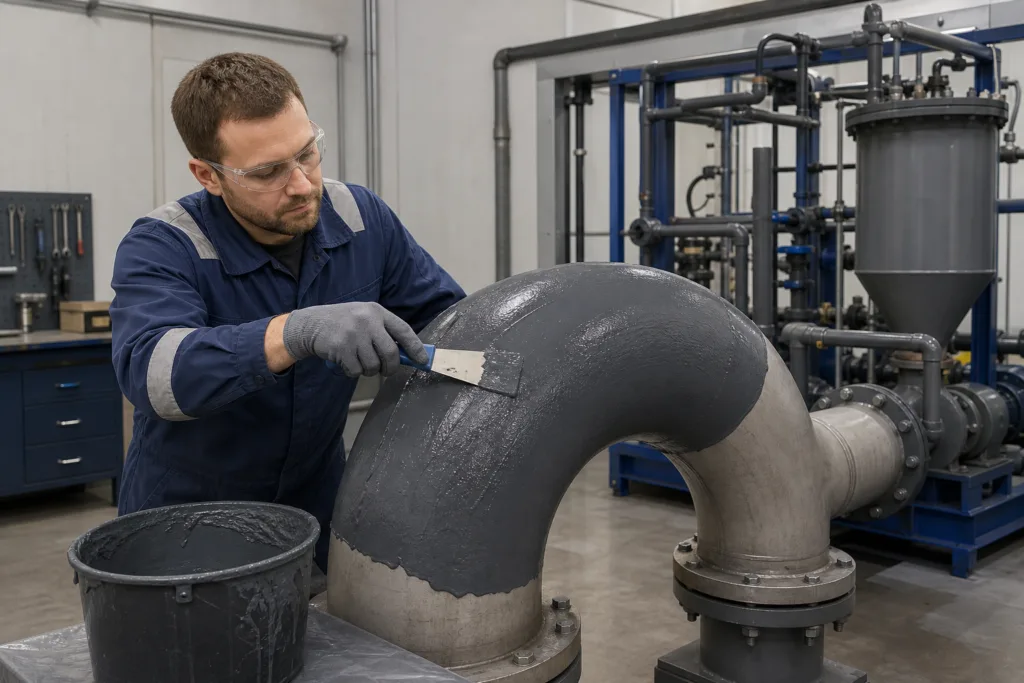
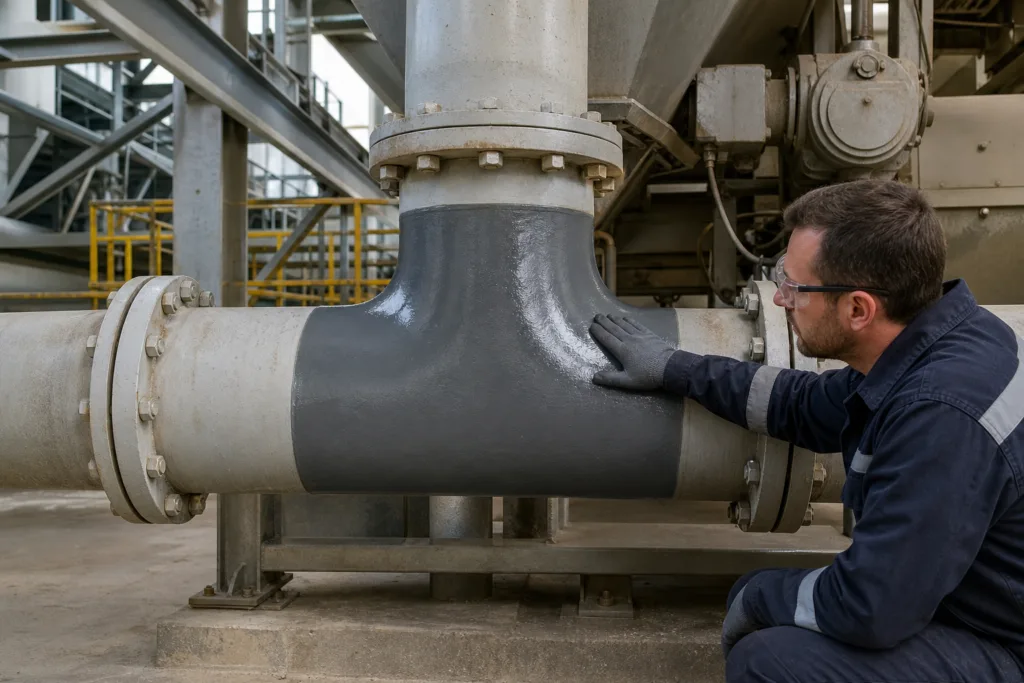
Pipe elbows and tees
Use ZDS-CA1841 as a protective coating on pipe elbows and tees exposed to abrasive slurry or bulk material flow. Its wear, erosion and cavitation resistance supports coating work where repeated particle or fluid action can damage the surface.
Industrial handling systems
Consider it for coating areas in slurry, powder, ash and bulk-material systems. The fit depends on the accessible area, the actual wear or fluid exposure and whether the operating temperature suits the compound.
Prepare the work surface
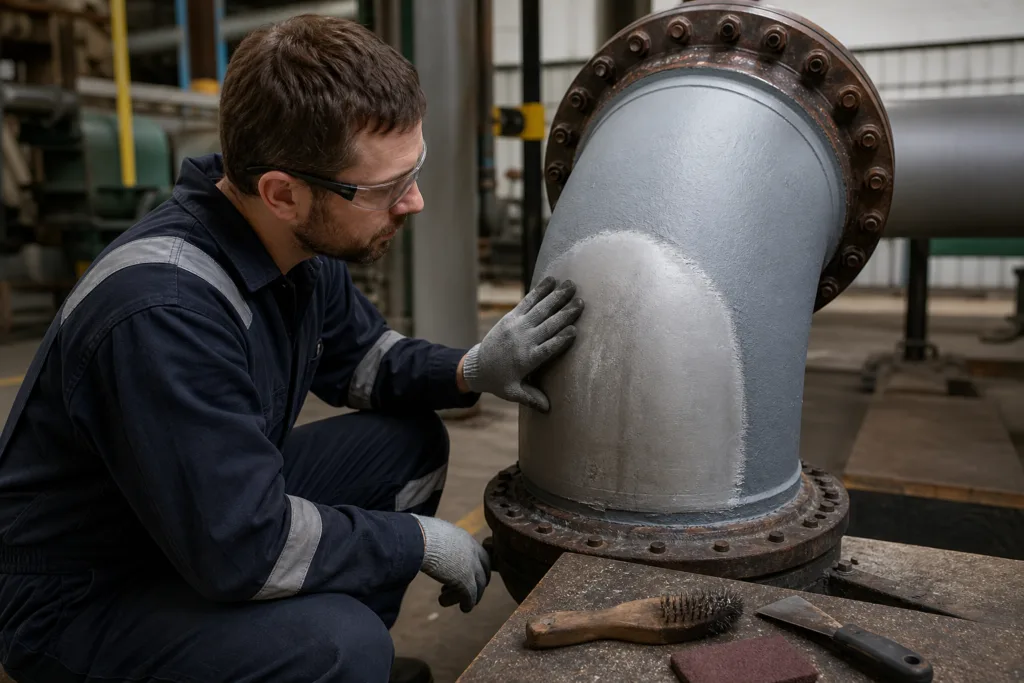
Prepare the coating area using the product-specific preparation instructions.
- Inspect the coating area for loose material, contamination and the condition of any existing surface layer.
- Arrange access to the full work area and the tools needed for the next step.
- Address contamination using the preparation method specified for this product and the actual surface.
Plan the work
Application and cure planning
- Prepare the coating area and arrange access and tools before starting.
- Mix the components according to the product instructions after surface preparation and setup are complete.
- Apply the coating or lining according to the product instructions and the recommended thickness where given.
- Use the technical table to plan the cure stages. Follow the applicable repair or application procedure for handling, loading and return to service.
Product selection questions
How much working time is available?
The typical working time at 25°C is 30-45 min. Complete surface preparation and setup before mixing.
What is the full-cure schedule?
Full cure: 24 h. Follow the product instructions for the applicable cure conditions.
What temperatures apply?
Recommended application temperature: 10°C to 35°C. Service temperature: -60 to 250°C. Application and service temperatures describe different conditions.
What thickness is recommended?
Recommended: 3-10 mm. Use the stated thickness type and range when planning the work.